Sale !
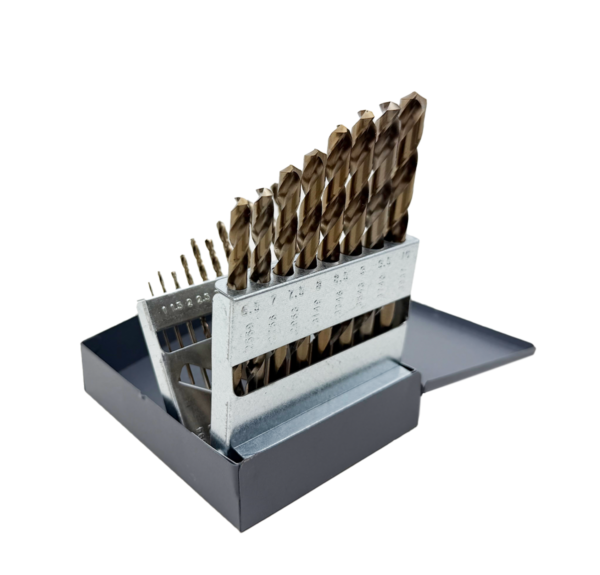
19pc Metric M42 Cobalt Jobber Drill Set, 1-10mm
Original price was: $219.98.$109.99Current price is: $109.99.
Super Sonic 19 piece M42 cobalt metric jobber drill set, 1.0 to 10.0 mm by 0.5 mm, with a 135 degree split point and gold finish in a two-tier steel index. Made to NAS 907J for stainless and other hard metals. Sold as a set.
The Super Sonic 19 piece metric set is 19 jobber length drills from 1.0 mm to 10.0 mm in 0.5 mm steps, ground from M42 cobalt high speed steel with a 135 degree split point and a gold finish. The drills are made to NAS 907J and come in a two-tier steel index. Made in the USA.
M42 has 8% cobalt, so it keeps its hardness at higher cutting temperatures than standard HSS. That makes this the set to reach for in stainless, high-temperature alloys, titanium and other hard, tough metals. The split point starts on center without a punch and cuts down on walking.
Features
- Super Sonic M42 cobalt, our private label
- 19 drills, 1.0 mm to 10.0 mm by 0.5 mm
- M42 cobalt high speed steel (8% cobalt)
- 135 degree split point, self-centering
- Jobber length, straight shank
- Gold finish
- Made to NAS 907J
- Two-tier steel index with marked sizes
- Made in the USA
Specifications
| Series | Super Sonic |
|---|---|
| Pieces | 19 |
| Size Range | 1.0 mm to 10.0 mm by 0.5 mm |
| Length | Jobber |
| Material | M42 cobalt HSS (8% cobalt) |
| Point | 135 degree split point |
| Finish | Gold |
| Shank | Straight |
| Specification | NAS 907J |
| Case | Two-tier steel index |
| Made In | USA |
Sizes in This Set
| Diameter | Decimal Inch | Flute Length | Overall Length |
|---|---|---|---|
| 1.0 mm | 0.0394″ | 17 mm (11/16″) | 41 mm (1-5/8″) |
| 1.5 mm | 0.0591″ | 22 mm (7/8″) | 48 mm (1-7/8″) |
| 2.0 mm | 0.0787″ | 25 mm (1″) | 51 mm (2″) |
| 2.5 mm | 0.0984″ | 35 mm (1-3/8″) | 60 mm (2-23/64″) |
| 3.0 mm | 0.1181″ | 41 mm (1-5/8″) | 70 mm (2-3/4″) |
| 3.5 mm | 0.1378″ | 45 mm (1-3/4″) | 73 mm (2-7/8″) |
| 4.0 mm | 0.1575″ | 54 mm (2-1/8″) | 83 mm (3-1/4″) |
| 4.5 mm | 0.1772″ | 56 mm (2-13/64″) | 86 mm (3-3/8″) |
| 5.0 mm | 0.1969″ | 62 mm (2-7/16″) | 92 mm (3-5/8″) |
| 5.5 mm | 0.2165″ | 64 mm (2-1/2″) | 95 mm (3-3/4″) |
| 6.0 mm | 0.2362″ | 70 mm (2-3/4″) | 102 mm (4″) |
| 6.5 mm | 0.2559″ | 73 mm (2-7/8″) | 105 mm (4-1/8″) |
| 7.0 mm | 0.2756″ | 73 mm (2-7/8″) | 105 mm (4-1/8″) |
| 7.5 mm | 0.2953″ | 78 mm (3″) | 111 mm (4-3/8″) |
| 8.0 mm | 0.3150″ | 81 mm (3-3/16″) | 114 mm (4-1/2″) |
| 8.5 mm | 0.3346″ | 87 mm (3-27/64″) | 121 mm (4-3/4″) |
| 9.0 mm | 0.3543″ | 89 mm (3-1/2″) | 124 mm (4-7/8″) |
| 9.5 mm | 0.3740″ | 92 mm (3-5/8″) | 127 mm (5″) |
| 10.0 mm | 0.3937″ | 95 mm (3-3/4″) | 130 mm (5-1/8″) |
Applications
- Metric holes in machine work, maintenance and repair
- Tap drills for common metric sizes, including 2.5 mm for M3 x 0.5, 5.0 mm for M6 x 1.0 and 8.5 mm for M10 x 1.5
- Clearance holes for metric fasteners
- Drill presses, mills, lathes and rigid magnetic drills
Materials
- Stainless steel
- High-temperature alloys
- Titanium
- Carbon and alloy steel
- Cast iron
- Certain plastics
Usage Notes
- Cobalt drills need a rigid setup with positive feed. A drill press or mill is best.
- Keep the feed steady in stainless. If the drill rubs, the material work hardens.
- Use cutting fluid in steel, stainless and titanium.
- Run slower speeds on the larger sizes and in harder material.
- Peck on deeper holes to clear chips.
Questions? Call DrillBitWarehouse.com at 800-350-8665.
| Weight | 1.9 lbs |
|---|